Why Lot-Level Traceability Matters After the Product Ships

Aug 28
Quality Records / Field Support

Why Lot-Level Traceability Matters After the Product Ships

When a unit returns from the field, a supplier identifies a suspect component lot, or a customer asks which revision was shipped, traceability stops being an abstract quality term. A useful lot record connects the affected product to its materials, process, inspection, test, configuration, and release evidence—so the response is based on facts rather than memory.

Field returns Material lots Test evidence Revision control
Linked Build Evidence Assembly 300-217 · Revision C
LOT / WO 28417
MATERIALLots & date codes
PROCESSTraveler & profile
VERIFYInspection & test
RELEASELabel & shipment
Field signalIdentify the lotRetrieve the evidence
Quick Answer

Traceability reduces uncertainty when the product is no longer on the manufacturing floor

Lot-level traceability does not guarantee that a product will never fail. Its value is that it helps an OEM determine what is affected, what is not affected, and which evidence should guide the response.

01

Narrow the scope

Identify which work order, material lot, revision, shipment, or configuration may be involved instead of treating every unit as equally suspect.

02

Compare the evidence

Look for common materials, process records, inspection findings, test results, or firmware versions across affected and unaffected assemblies.

03

Protect unaffected product

Evidence-based containment can prevent a broad hold, return, or reinspection when the actual risk is limited to a smaller population.

04

Improve the next build

Field information can be connected back to design, sourcing, process, inspection, test, and documentation decisions that should change going forward.

The Traceability Chain

A useful lot record connects six parts of the build story

Traceability is not one spreadsheet or one label. It is the relationship between identifiers and records that lets a team move from a shipped assembly back through the decisions and evidence behind it.

After the Product Ships

The value appears when an unexpected question has to be answered quickly

These scenarios are different, but each depends on being able to connect a product in the field to the right manufacturing evidence without reconstructing the history from scattered emails and memory.

Field Return

One unit develops an intermittent failure

The investigation can compare that unit or lot with nearby builds, review materials and test records, and determine whether the condition appears isolated or patterned.

Supplier Alert

A manufacturer identifies a suspect component population

Lot or date-code linkage can help determine which assemblies used the affected material, where they shipped, and whether containment is necessary.

Configuration Question

A firmware or revision mismatch is reported

Programming logs, assembly revision, label data, and shipment records can distinguish a software configuration issue from an assembly-process problem.

Customer Evidence

An audit, service event, or corrective action needs support

Linked records help show what was built, which requirements applied, what was verified, and how affected product was identified and controlled.

Choose the Right Granularity

Lot-level and unit-level traceability answer different questions

More data is not automatically better. The right approach depends on product risk, end market, service model, customer requirements, regulation, quantity, test architecture, and the cost of capturing and retaining the records.

Lot-Level Traceability

Connects a defined group of assemblies to shared build evidence

Lot-level records are often practical for high-mix, low-volume programs where units share materials, process, inspection, and release history under a work order or production lot.

  • Efficiently narrows material, process, revision, and shipment scope
  • Supports repeat-build history and field-return comparisons
  • Can be tailored to critical parts or processes rather than every data point
  • May not distinguish every unit when individual configuration varies
Unit-Level Traceability

Connects a unique serial number to per-unit evidence

Unit-level records add granularity when each product may have unique programming, calibration, test values, configuration, or service history.

  • Supports per-unit programming and functional-test logs
  • Helps isolate serial-specific configuration or performance questions
  • May be appropriate for regulated, safety-related, or service-intensive products
  • Requires an identifier, data capture, retrieval, and retention plan

A layered approach is often the best answer

An OEM may use lot-level traceability for the overall build, enhanced material tracking for selected critical components, and unit-level serialization for programming or final-test results. The scope should be defined before launch so quoting, labeling, systems, and work instructions all support the same plan.

The Investigation Path

From a field signal to a controlled answer

Good traceability does not replace failure analysis. It gives the investigation a reliable starting point and helps the team compare the right populations instead of searching blindly.

Capture the exact signal

Record the symptom, environment, operating time, serial or label information, return condition, photos, logs, and any known history.

Identify the unit or lot

Use the serial, lot label, work order, shipment record, customer order, or product revision to define the population being investigated.

Retrieve linked evidence

Pull the build traveler, material records, deviations, process references, inspection results, test data, firmware, and release documentation.

Compare affected and unaffected product

Look for shared lots, dates, revisions, suppliers, processes, test values, programming images, operators, or shipment groups that may explain the pattern.

Contain only what the evidence supports

Hold, inspect, notify, or recover the appropriate population while avoiding unnecessary disruption to product that is demonstrably outside the scope.

Close the loop

Document the finding, update corrective actions, revise the BOM or process where needed, and preserve the decision so the next build benefits.

Practical Record Checklist

What a useful lot-level record may include

Not every program needs every item below. The list is a planning tool for deciding which evidence must remain linked to the lot after shipment.

  • Assembly part number, description, and released revision
  • Customer purchase order, work order, traveler, and build dates
  • Bare PCB revision, fabrication lot, or supplier identification as required
  • Critical component manufacturer part numbers, sources, and lot/date codes as scoped
  • Approved substitutions, deviations, waivers, and engineering-change status
  • Solder alloy, paste or flux identity, and relevant special-process materials
  • Process route, signoffs, rework records, and reflow-profile reference where required
  • AOI, X-ray, visual-inspection, or first-article report references
  • ICT, flying-probe, functional-test, calibration, or burn-in results
  • Firmware revision, programming verification, and unique identifiers where applicable
  • Final label, serialization, acceptance, certificate, or report package
  • Shipment date, quantity, destination, packing reference, and retained sample status if specified

Micron’s quality capabilities include component-to-board traceability and build records tied to program requirements, while its Testing & Programming services can include lot-level reports, per-unit pass/fail data, programming verification, and traveler linkages.

Records Are Not Enough

Traceability has to work under pressure

A company can collect large amounts of data and still struggle during a field investigation. The record system is useful only when identifiers remain connected and the evidence can be found, understood, and trusted.

Linked

Use common identifiers across records

The lot, work order, traveler, serial, report, and shipment should reference one another instead of existing as unrelated documents.

Retrievable

Plan how evidence will be found later

File names, databases, labels, report formats, permissions, and backups should support a practical search years after the build.

Proportionate

Capture the data the program actually needs

Risk-based traceability avoids both extremes: too little evidence to investigate and uncontrolled data collection with no clear purpose.

Controlled

Protect revisions, exceptions, and retention

Records should show which requirements applied, who approved changes, how long data is retained, and how corrections are handled.

Plan It Before the Build

Six questions to answer during RFQ and launch

Traceability affects labels, travelers, receiving, production systems, inspection, testing, programming, reporting, record retention, and price. It is much easier to design the path before the first lot is released.

Industry Reference

A risk-based framework is better than a generic promise

IPC-1782 addresses manufacturing and supply-chain traceability

The Global Electronics Association describes IPC-1782 as a framework for traceability based on perceived risk and agreement between the user and supplier. That principle is important: traceability scope should be explicit, proportional, and connected to the end-use need rather than assumed.

Review the IPC-1782 overview
Related Micron Capabilities

Traceability is strongest when material control, assembly, inspection, test, programming, release, and customer documentation are planned as one connected system.

Frequently Asked Questions

Questions OEM teams ask about traceability

Is lot-level traceability the same as serialization?

No. Lot-level traceability connects a defined group of assemblies to shared build evidence. Serialization gives each unit a unique identifier. A program can use lot-level traceability without individual serial numbers, or combine both when per-unit configuration, test, calibration, or service history matters.

Does every component need lot or date-code tracking?

Not necessarily. The appropriate scope depends on customer requirements, product risk, regulation, availability concerns, and the likely use of the data. Some programs track all components; others focus on bare boards, semiconductors, safety-critical items, customer-supplied material, or selected high-risk parts.

Can traceability be added after a build is complete?

Only to the extent that reliable source records already exist. Labels, lot relationships, material identity, programming logs, and per-unit test results cannot always be reconstructed after production. The safest approach is to define the required identifiers and records before launch.

How long should traceability records be retained?

Retention should be agreed based on the customer contract, end market, regulatory requirements, warranty or service period, product life, and the practical value of the records. The period and format should be defined before the build rather than assumed.

What should we include in an RFQ if traceability matters?

Describe whether you need lot-level or unit-level records, which materials and processes must be traced, required label or serial formats, inspection and test reports, programming logs, retention periods, customer templates, certificates, and any special approval path for deviations or substitutions.

Define the Evidence Before Production

Tell Micron what you may need to prove after shipment

Share the assembly files, quantities, end-use context, labeling needs, test plan, programming requirements, critical materials, report expectations, and retention requirements. Micron can help align the traceability scope with the build path before production begins.
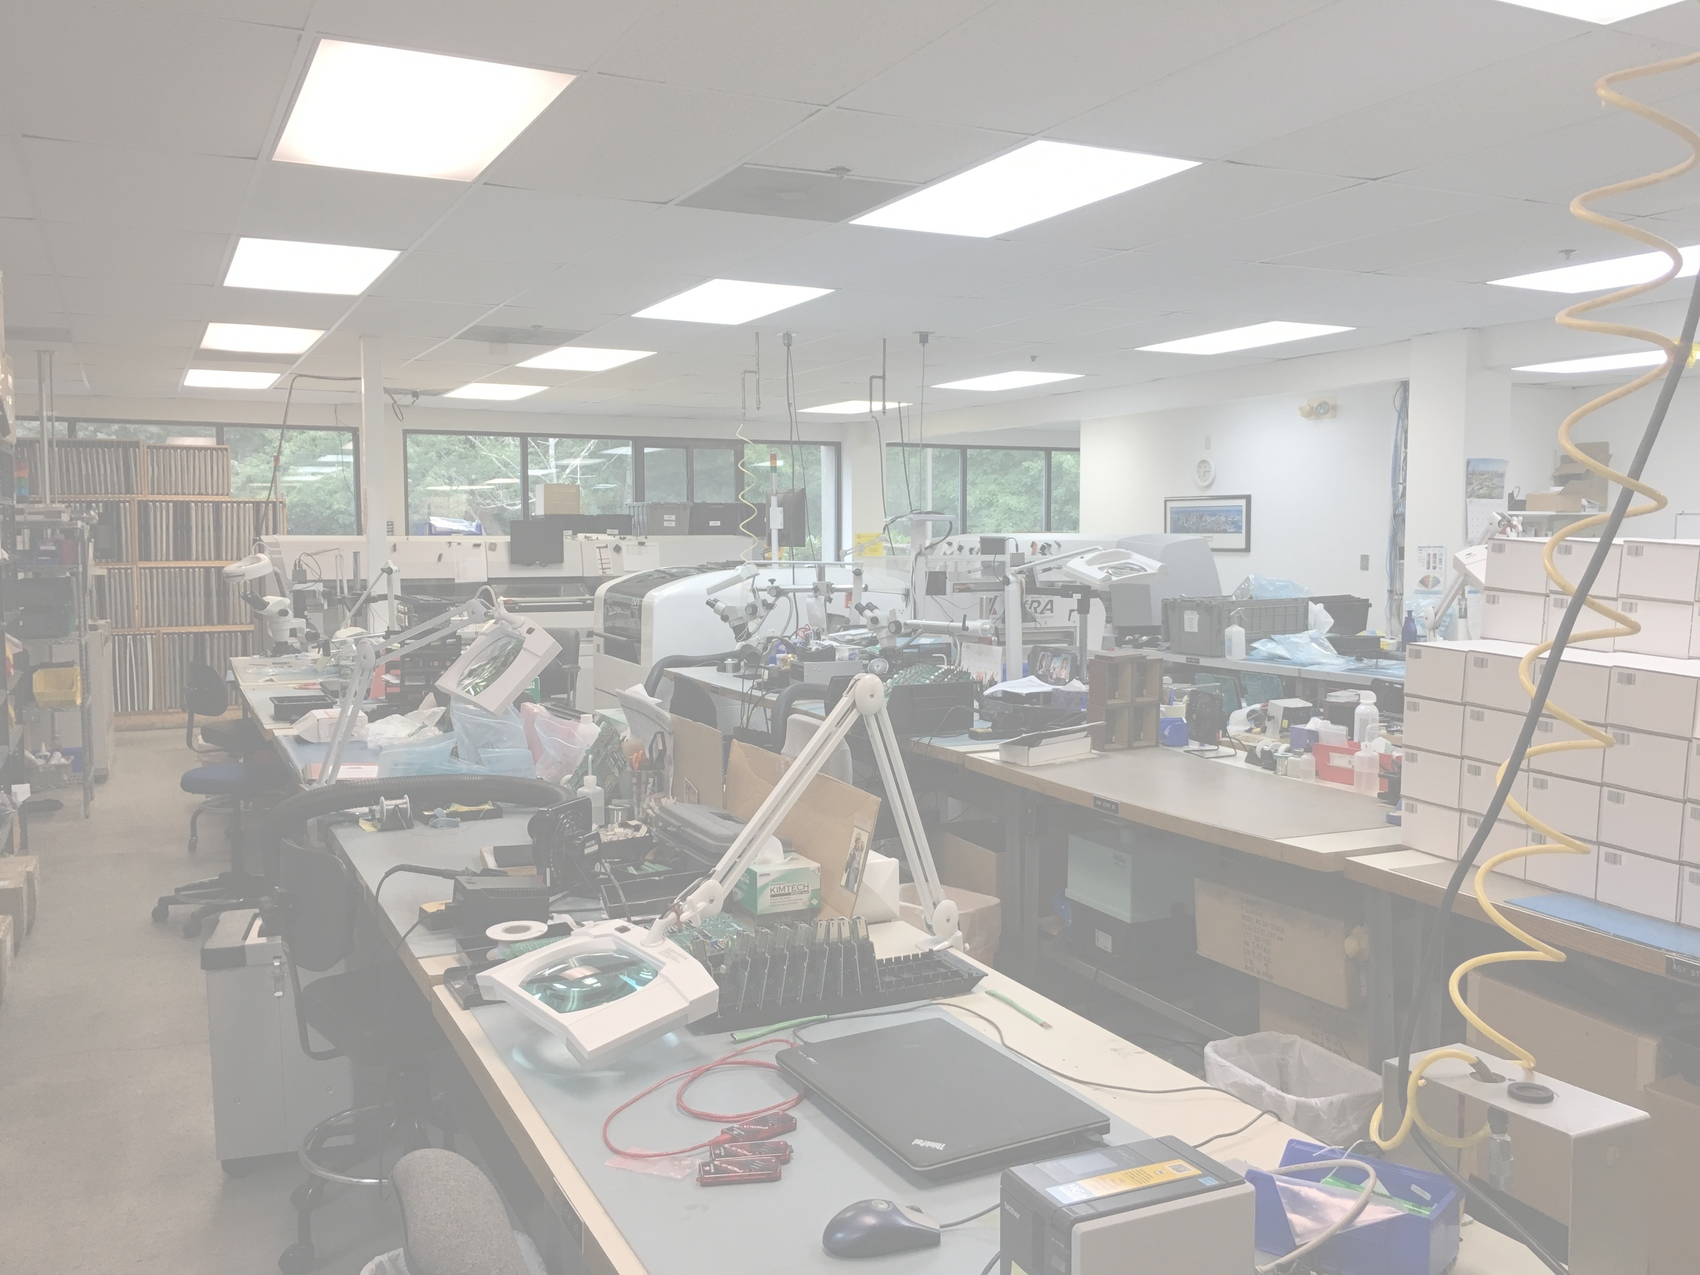
A PCB Assembly’s Journey Through the Micron Floor

Aug 14
Inside Micron / EMS Process

A PCB Assembly’s Journey Through the Micron Floor

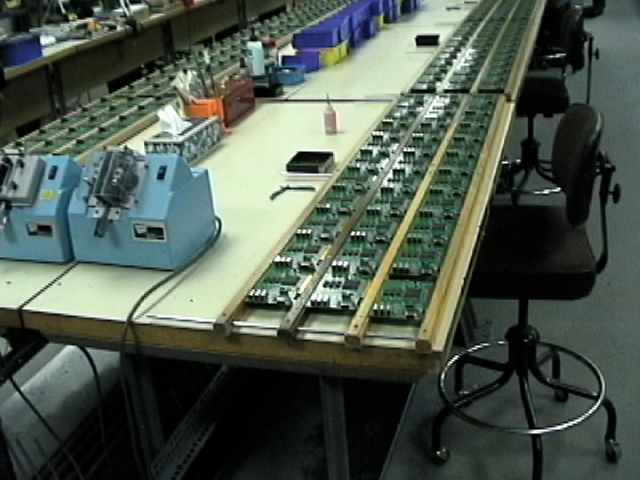
A finished assembly does not move directly from a box of components to shipment. It follows a planned route through documentation review, material control, SMT or Through Hole assembly, inspection, test, and final release—with each handoff protecting the design intent.

Norwood, Massachusetts SMT + Through Hole Inspection + test Documented release
One connected manufacturing path

From design data to a documented shipment

01Review & launch
02Materials & kit control
03SMT assembly
04Through Hole & integration
05Inspection & test
06Release & shipment
The Big Picture

The route is controlled, but it is not one-size-fits-all

A prototype, a mixed-technology control board, and a repeat production assembly may pass through many of the same departments, but they do not necessarily need the same process, inspection coverage, test plan, or records. The route should match the product and the customer’s requirements.

The physical route

Where the board goes

Receiving, preparation, stencil printing, placement, reflow, secondary assembly, inspection, test, cleaning, packaging, and shipment as the build requires.

The information route

What travels with it

Revision-controlled files, traveler instructions, inspection criteria, programming details, test results, labels, serial information, and customer-specific records.

Six-Stage Journey Map

Six connected stages, with checks at every handoff

The exact routing can change by program. What should not change is the discipline used to confirm the current revision, control materials, follow the build plan, verify workmanship and function, and close the record before shipment.

Review & launch

Confirm the build package, revision, sourcing model, quantities, schedule, workmanship requirements, test intent, and special instructions.

Materials & kit control

Receive and identify boards, components, stencils, hardware, and customer-supplied material; surface shortages or discrepancies before the build starts.

SMT assembly

Print solder paste, place components, run a controlled reflow profile, and inspect the assembly using the coverage defined for the program.

Through Hole & integration

Add connectors, switches, power parts, hardware, wiring, or enclosure content through hand, wave, mixed-technology, and electromechanical operations.

Inspection, test & programming

Apply AOI, X-ray, visual inspection, electrical test, functional test, firmware loading, or serialization according to the approved scope.

Final release & shipment

Complete final checks, close travelers and records, verify labels and packaging, then release the assembly for protected shipment.

From the Micron Floor

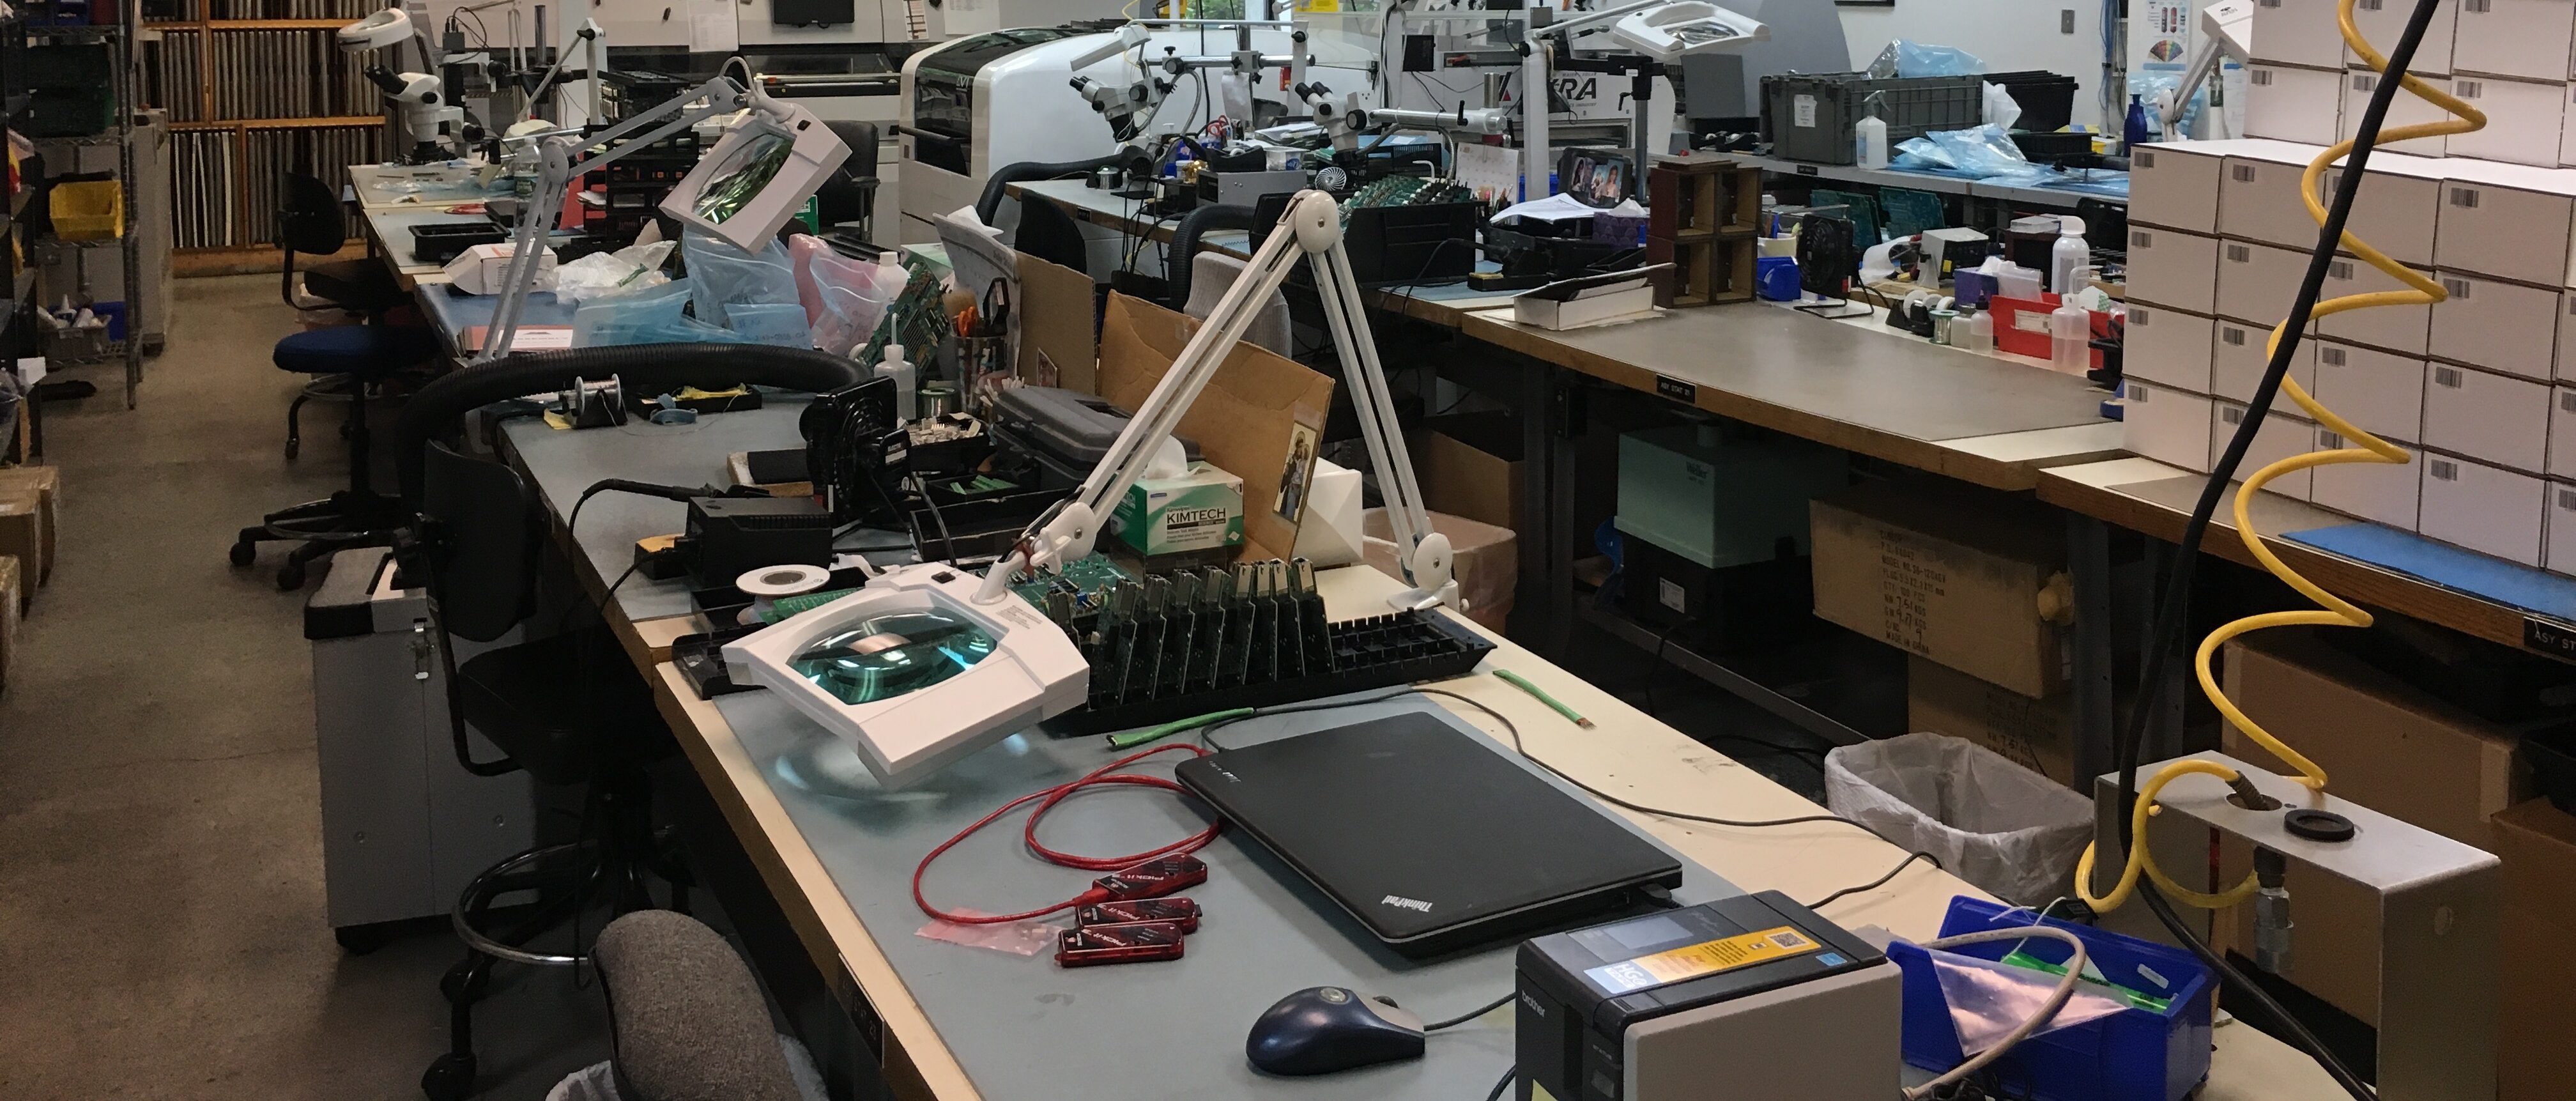
The work moves from automated precision to skilled hands

Modern PCB assembly is not purely automated and it is not purely manual. The strongest manufacturing path uses each where it adds value: controlled equipment for repeatable process steps, experienced technicians for mixed technology and secondary operations, and clear inspection and test criteria throughout.

Equipment Along the Path

The core equipment connects print, placement, heat, inspection, and Through Hole work

Equipment does not replace process discipline. It makes a defined process repeatable. Programming, setup verification, profiling, inspection criteria, and trained review still determine how effectively each machine supports the build.

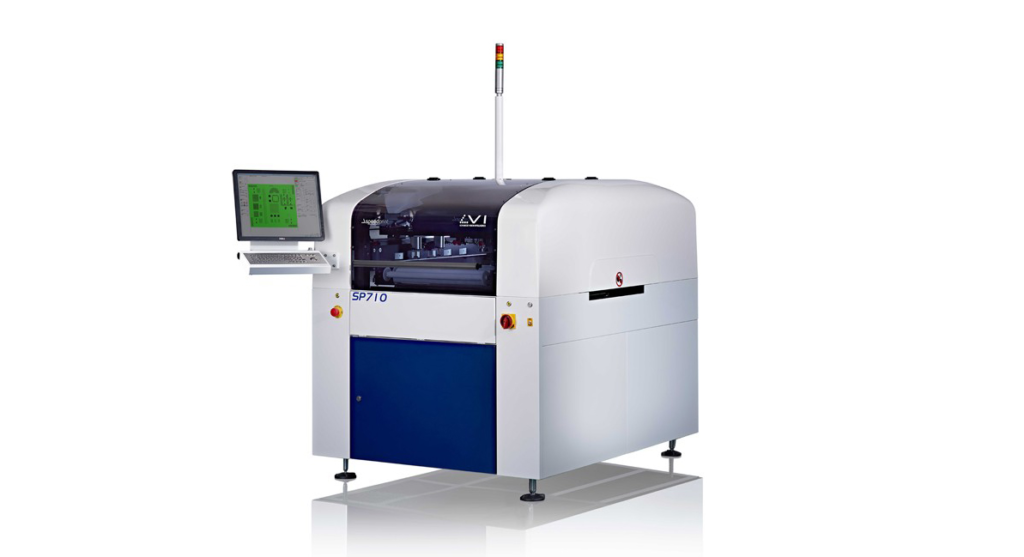
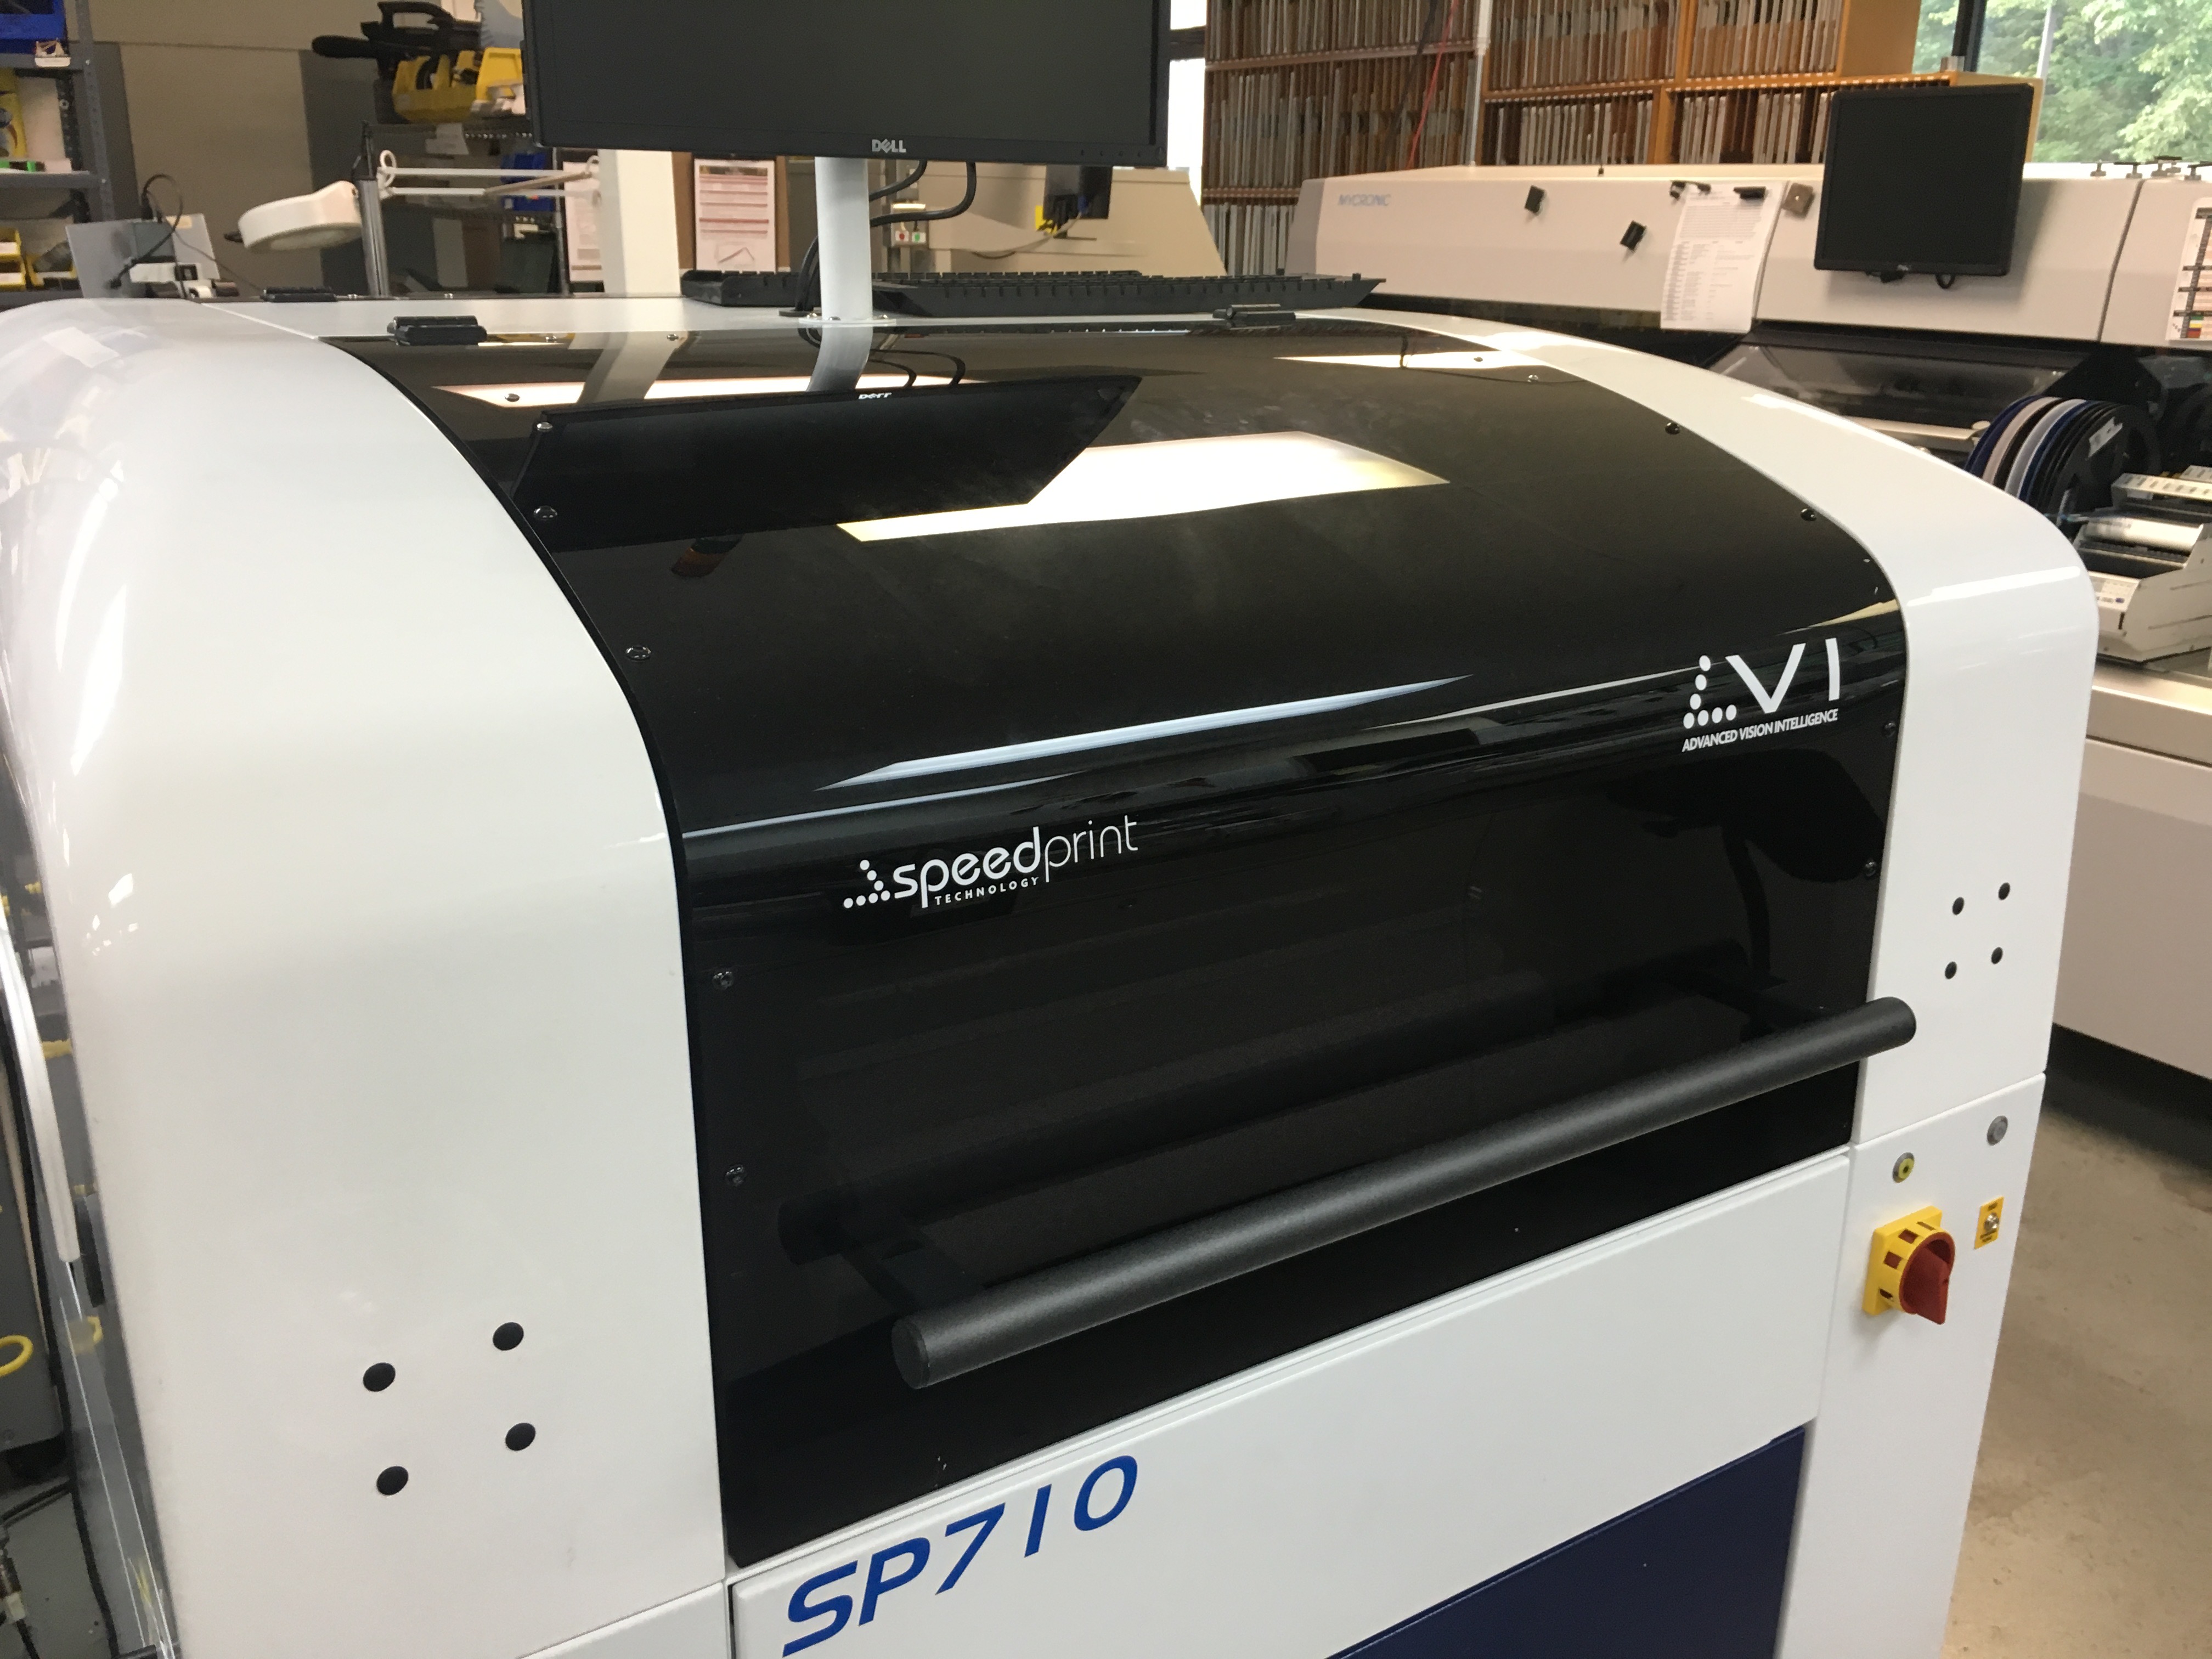
SpeedPrint SP710 stencil printer used for solder paste printing
Print

SpeedPrint SP710

Precise stencil-to-board alignment supports consistent solder paste deposition before component placement.

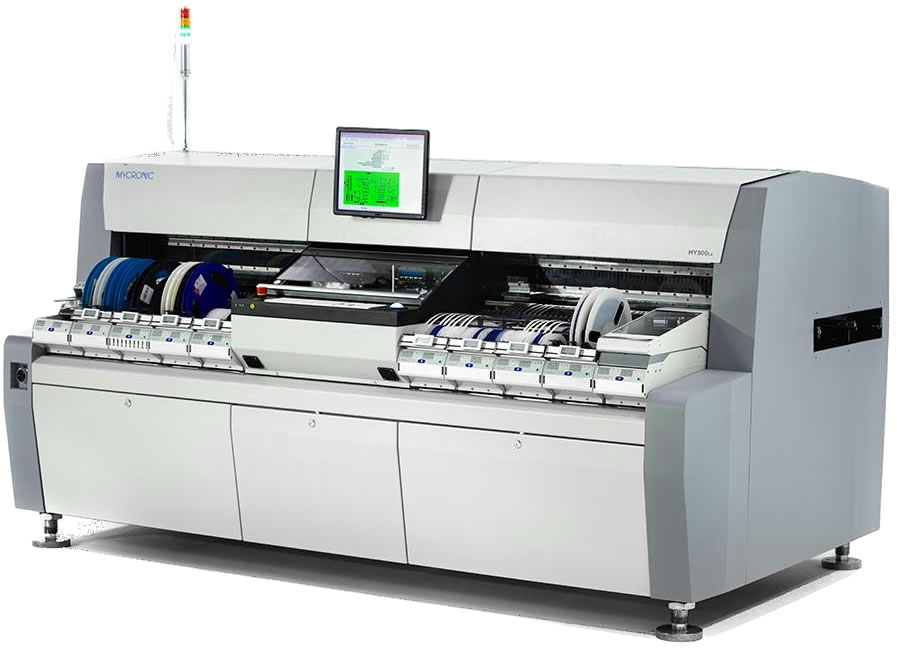
Mycronic MY300 pick-and-place equipment used for SMT component placement
Place

Mycronic MY300 & MY200

Vision-guided placement supports fine-pitch packages, QFN, BGA, and small passive components.

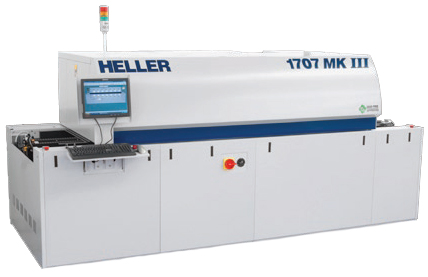
Heller 1707 MKIII reflow oven used in the SMT assembly process
Reflow

Heller 1707 MKIII

Controlled multi-zone profiles help form repeatable solder joints across assemblies with different thermal demands.

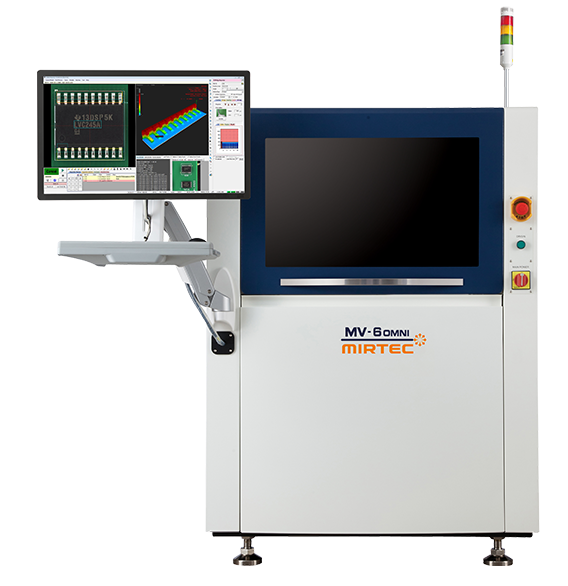
Mirtec MV-6 Omni 3D automated optical inspection system
Inspect

Mirtec MV-6 Omni 3D AOI

Three-dimensional optical inspection helps evaluate placement, polarity, component presence, and visible solder conditions.

Wave soldering system used for Through Hole PCB assembly
Through Hole

Controlled wave soldering and skilled hand assembly

Through Hole work may use wave soldering, selective hand soldering, fixtures, and technician-controlled operations based on the board geometry, component mix, volume, and workmanship requirements.

Explore Micron’s Through Hole capabilities

The Detailed Route

What happens as the assembly moves through the floor

The stages below describe the connected manufacturing logic. Individual projects may add first-article holds, special processes, customer approvals, coating, calibration, burn-in, or other program-specific gates.

Project review and launch planning

The build begins with a review of what is being made and how success will be measured. The team aligns the BOM, Gerbers or ODB++, pick-and-place data, assembly drawings, revision level, quantities, schedule, sourcing model, solder requirements, inspection scope, programming, test, labels, and records.

  • Resolve mismatched revisions and unclear assembly notes before production
  • Identify DFM, material, stencil, panel, test-access, or special-process questions
  • Prepare the traveler, route, and customer-specific instructions

Receiving, material verification, and kit readiness

Turnkey, consigned, and hybrid builds all depend on knowing what has arrived, what matches the BOM, and what is still missing. Components, bare boards, stencils, hardware, and customer-supplied materials are identified and routed for the build.

  • Confirm line items, quantities, part identity, board revision, and kit status
  • Surface shortages, damaged material, substitutions, and open approvals
  • Apply appropriate ESD and moisture-sensitive handling controls

SMT programming, printing, placement, and reflow

For surface-mount work, the production path connects stencil printing, feeder and placement setup, component verification, and profile-controlled reflow. Each stage depends on accurate data and a setup that matches the released assembly.

  • Apply solder paste with controlled alignment and print consistency
  • Program and verify component locations, rotations, packages, and polarity
  • Use a thermal profile appropriate to the board, paste, and component mix

See Micron’s SMT assembly process and equipment.

Through Hole, secondary operations, and electromechanical integration

After SMT—or as the primary route for some assemblies—connectors, switches, relays, transformers, power parts, mechanical hardware, wires, and other odd-form components may be installed. Some projects continue into subassemblies or finished enclosures.

  • Coordinate manual insertion, hand solder, wave solder, lead trim, and hardware
  • Verify orientation, mechanical fit, solder quality, and mixed-technology sequencing
  • Add wiring, harnesses, labels, torque-controlled hardware, and enclosure content as specified

Related capabilities: Through Hole assembly and electromechanical assembly and box build.

Inspection, electrical test, programming, and feedback

Inspection confirms workmanship; test confirms electrical or product behavior. The appropriate combination depends on component types, access, risk, volume, and what the customer needs the assembly to prove before shipment.

  • Use AOI and visual inspection for visible placement and workmanship conditions
  • Use X-ray where hidden solder joints or internal conditions require review
  • Apply ICT, flying-probe, functional test, programming, serialization, and result capture as scoped

Explore Micron’s testing and programming capabilities.

Final inspection, documentation closeout, packaging, and shipment

Release is the final manufacturing gate, not an administrative afterthought. The assembly, records, labels, test status, and packaging should all agree with the program requirements before the order leaves the floor.

  • Confirm final workmanship, cleaning, labels, serialization, and configuration
  • Close travelers, inspection records, test results, programming logs, and required reports
  • Use protective ESD-safe packaging and customer-specific pack-out as required
Where the Route Changes

The same floor supports different manufacturing strategies

The physical equipment may be familiar from one job to the next, but the decisions around setup, hold points, inspection, test, documentation, and release can be very different.

Prototype / NPI

Learn quickly and capture findings

First articles may include additional review, DFM feedback, engineering questions, controlled rework, ECO intake, test development, and documentation intended to support the next build.

Repeat Production

Repeat an approved process reliably

Stable builds depend on released revisions, repeatable setup data, approved materials, defined acceptance criteria, established test coverage, and a clear response when something changes.

Mixed Technology

Coordinate SMT, Through Hole, and mechanics

The route must account for component height, thermal mass, solder sequence, washing, fixtures, hand access, inspection access, hardware, wiring, and final integration.

High-Reliability Programs

Plan the evidence before the build

Customer-defined IPC class, traceability, archived profiles, inspection records, test data, serialization, labeling, and retention requirements should be aligned during launch.

Keep the Journey Moving

What customers can provide before the build reaches the floor

A complete package helps, but it does not need to be perfect to start the conversation. The most important step is to distinguish released requirements from assumptions and details that are still changing.

  • BOM with manufacturer part numbers, alternates, quantities, DNP notes, and revision
  • Gerbers or ODB++, fabrication notes, panel details, and board revision
  • Pick-and-place or centroid data with correct rotations and board side
  • Assembly drawings, polarity notes, mechanical drawings, and special instructions
  • Target quantities, schedule goals, and prototype, pilot, or production context
  • Turnkey, consigned, or hybrid material preference and any customer-supplied parts
  • IPC class, solder type, cleaning, coating, labeling, serialization, and packaging needs
  • Test intent, firmware, fixtures, pass/fail criteria, reports, and traceability requirements
Explore the Build Path

Use these pages to look more closely at the manufacturing stages described in this journey.

Start the Journey

A reliable build starts before the first board reaches the line

Share the design package, quantities, sourcing preferences, test needs, and what is still changing. Micron can help identify the route from quote review to a controlled, inspectable, and repeatable assembly.

Choosing an EMS Partner for Medical & Life Sciences

Aug 07
Medical & Life-Science Electronics

What Medical and Life-Science OEMs Should Look for in an EMS Partner

For research instruments, diagnostic subassemblies, patient-adjacent electronics, and regulated programs, manufacturing capability is only the starting point. The right EMS partner must also manage evidence, change, risk, test, and communication with discipline.

Documentation Traceability Testing Local support
What a medical and life-science electronics program needs from an EMS partner Four equal cards for documentation, traceability, verification, and communication feed a path from research need through prototype and pilot to repeatable production. WHAT STRONG PROGRAMS CONNECT DOCUMENTATION Current revisions and build records TRACEABILITY Materials, lots, serials, and history VERIFICATION Inspection, test, and programming COMMUNICATION Fast decisions and direct access RESEARCH PROTOTYPE PILOT REPEATABLE Scientific urgency + manufacturing discipline
Quick Answer

Choose an EMS partner that can preserve design intent as the program changes

Medical and life-science electronics rarely move in a perfectly straight line. Research findings, clinical feedback, component availability, test results, and regulatory strategy can all affect the build. A strong partner helps the OEM move quickly without losing control of revisions, materials, acceptance criteria, or production records.

01

Program-stage fit

The manufacturer should understand the difference between a research prototype, an NPI pilot, and a controlled repeat-production build.

02

Documentation discipline

BOMs, drawings, firmware, travelers, test procedures, and acceptance criteria need clear revisions and controlled handoffs.

03

Traceability

Material lots, serial numbers, programming data, inspection records, and customer-defined history should be captured at the level the program requires.

04

Verification strategy

Inspection, electrical test, functional test, firmware loading, and fixture plans should be considered before the build reaches final assembly.

05

Change control

The EMS partner should have a practical method for handling ECOs, substitutions, rework, deviations, and updated instructions.

06

Responsive communication

When a design is evolving, direct access to the people reviewing, sourcing, building, inspecting, and testing the assembly can be a major advantage.

Start With the Actual Program

“Medical” can describe very different manufacturing requirements

The right manufacturing approach depends on what the electronics do, where they will be used, who controls the quality system, and how mature the design is. A research-use instrument and a commercially distributed finished medical device may share components, but they do not automatically share the same supplier requirements.

Research & Proof of Concept

Fast learning with controlled revisions

Early builds may prioritize engineering access, modest quantities, specialized interfaces, and rapid design changes. Even here, preserving the BOM, firmware, test notes, and build history makes the next iteration more useful.

Laboratory Instrumentation

Repeatability, calibration, and serviceability

Benchtop systems and analytical instruments may require stable power, low-noise assembly, defined calibration steps, firmware control, test logs, and long-term component planning.

Diagnostic Subassembly

Defined interfaces and evidence

PCB assemblies used inside a larger diagnostic platform may need customer-specific lot traceability, functional verification, labeling, cleanliness, serialization, and controlled acceptance criteria.

Finished Regulated Device

Explicit regulatory and supplier controls

If the program requires ISO 13485 certification, FDA Quality Management System Regulation alignment, or another specific quality-system qualification, verify that requirement directly during supplier selection.

!

Do not treat “medical capable” as a substitute for supplier qualification

General electronics capability, IPC workmanship, ESD controls, or traceability can be important—but they are not automatically equivalent to a program-specific certification or regulatory quality-system requirement. Define what the product and your supplier controls actually require.

What to Evaluate

Eight capabilities that matter beyond component placement

A capable line is important. The stronger differentiators are often found in how the EMS partner prepares the build, manages information, verifies the result, and responds when something changes.

Experience moving from prototype to repeat production

A prototype proves that a design can be built. Production requires repeatable sourcing, approved processes, stable documentation, test coverage, and a record of what changed. Look for an EMS partner that can support Prototypes & NPI without treating the first successful board as the end of the launch process.

Early DFM and DFT feedback

Footprints, component orientation, thermal relief, stencil strategy, panelization, test access, programming headers, and fixture needs are easier to improve before the design is frozen. A partner that asks useful questions early can prevent expensive rework later.

Revision control that reaches the manufacturing floor

The current BOM, Gerbers or ODB++, pick-and-place data, assembly drawings, firmware, test procedure, and labeling instructions should agree. The key question is not whether a document system exists—it is whether operators and inspectors are using the correct information at the correct step.

Material controls and traceability matched to risk

Ask how the partner handles customer-supplied kits, approved vendor lists, moisture-sensitive devices, ESD-sensitive components, date or lot codes, authorized sourcing, substitutions, shortages, and unused inventory. Traceability should be defined—not assumed.

Inspection, test, and programming as one connected plan

AOI and X-ray answer different questions from ICT or functional test. Firmware loading and serialization can also be production-critical. Review the intended coverage, fixture ownership, pass/fail criteria, data retention, and failure-handling path before launch. Micron’s Testing & Programming capabilities support these discussions.

A controlled path for ECOs, deviations, and rework

Medical and life-science programs often evolve. The EMS partner should be able to identify which revision was built, document authorized deviations, separate engineering changes from purchasing substitutions, and prevent old instructions from remaining active.

Supply-chain planning for long program lives

Laboratory and medical electronics may remain in service for years. BOM scrubs, approved alternates, lifecycle reviews, last-time-buy planning, and transparent sourcing assumptions can reduce the chance that a mature design becomes unbuildable because one component changes status.

Direct communication with accountable people

When an engineer has a test question or a researcher changes a connector, long handoff chains create delay. A responsive EMS model gives the OEM access to project management, sourcing, manufacturing, and quality personnel who understand the specific build.

The Massachusetts Advantage

Research teams often need a nearby manufacturing conversation—not just a purchase order

Massachusetts brings hospitals, universities, research laboratories, device developers, diagnostics companies, and specialized suppliers into a dense life-sciences ecosystem. For evolving electronics programs, proximity can make design reviews, bring-up support, fixture discussions, and change decisions more practical.

Micron has experience supporting electronics projects for research teams associated with area hospitals and research institutions. Without identifying confidential programs, those engagements have reinforced a recurring lesson: research groups need speed, but the value of each build increases when decisions, revisions, test results, and assembly history remain organized enough to support the next experiment—or the next stage of commercialization.

Research Team

Define the scientific need

Share the intended use, current design maturity, critical interfaces, expected changes, quantities, and what the electronics must prove.

EMS Collaboration

Translate intent into a build plan

Review files, material strategy, manufacturability, test intent, documentation, and the practical path from prototype to pilot.

Controlled Result

Return more than assembled boards

Deliver a build whose revision, materials, inspection, programming, test, and lessons learned can support the next decision.

Evidence, Not Assumptions

Define what records the program should produce

Not every build needs every record. The important step is deciding what evidence matters before production begins, then making sure the traveler, inspection, test, and shipment process can produce it.

R

Revision record

Which BOM, PCB data, assembly drawing, firmware, test procedure, and labeling instructions were used?

M

Material history

Which manufacturer part numbers, lots, date codes, approved alternates, or customer-supplied materials entered the build?

I

Inspection results

Were first article, AOI, X-ray, visual inspection, workmanship, or customer-specific checkpoints required and recorded?

T

Test and programming data

What was programmed, which fixture or procedure was used, what passed, and how were failures handled?

C

Change authorization

Who approved deviations, substitutions, rework, ECO implementation, or acceptance of a nonstandard condition?

S

Shipment documentation

Define serial lists, certificates, labels, test summaries, packaging, ESD protection, and any customer-required release records.

A Practical Qualification Path

Evaluate the partner against the build you actually intend to run

Certifications, equipment lists, and capability statements are useful screening tools. A pilot build shows how the relationship works when real files, materials, questions, and acceptance criteria enter the process.

Define program requirements

Clarify product stage, intended use, quality-system obligations, IPC class, traceability, test, records, quantities, and schedule.

Review the build package

Use the BOM, Gerbers or ODB++, assembly drawings, firmware, test notes, and risk areas to evaluate technical fit.

Run a representative pilot

Include the documentation, inspection, programming, test, labeling, and reporting expected in later builds.

Review the evidence and handoff

Confirm what was learned, what changed, which records were produced, and what must be stabilized before repeat production.

Partner Checklist

Questions to ask before sending a medical or life-science electronics RFQ

The answers should be specific to your build—not generic assurances. Use this list to structure the first technical and sourcing conversation.

  • Can you support our current stage: research prototype, NPI, pilot, or recurring production?
  • How do you confirm that the BOM, PCB files, drawings, firmware, and test procedure are on the same revision?
  • What DFM and DFT feedback is available before the build is released?
  • How are customer-supplied materials, moisture-sensitive parts, ESD controls, and approved alternates handled?
  • What lot, date-code, serial, programming, and inspection traceability can be retained?
  • Which AOI, X-ray, ICT, flying-probe, functional-test, or programming steps are appropriate for this design?
  • Who owns test fixtures, software, calibration, maintenance, and pass/fail criteria?
  • How are ECOs, deviations, rework, substitutions, and nonconforming material authorized and documented?
  • What certifications or quality-system requirements does our program require, and can the supplier meet them?
  • Who will communicate with our engineering, research, purchasing, and quality teams when a question arises?
  • Can the supplier support both SMT Assembly and Through Hole Assembly if the design is mixed-technology?
  • What records and packaging will accompany the shipment, and how long will production data be retained?
Useful External References

Industry context and regulatory resources

These authoritative resources provide useful context for Massachusetts life sciences, U.S. medical-device quality systems, and electronics manufacturing standards.

Massachusetts Life Sciences Center

The MLSC describes Massachusetts as a global life-sciences hub and provides resources covering the Commonwealth’s research, innovation, infrastructure, and manufacturing ecosystem.

Explore the Massachusetts ecosystem

FDA Quality Management System Regulation

The FDA’s QMSR became effective February 2, 2026 and incorporates ISO 13485:2016 by reference for applicable finished-device manufacturers. OEMs should determine how those requirements affect their own supplier controls and manufacturing program.

Review the FDA QMSR

IPC / Global Electronics Association standards

IPC standards provide widely used expectations for electronics assembly workmanship, soldering, documentation, and manufacturing consistency.

View IPC standards resources
Frequently Asked Questions

Questions medical and life-science OEMs often ask

Does every medical or life-science electronics program require an ISO 13485-certified EMS provider?

No single answer applies to every project. Requirements depend on the product, intended use, regulatory status, customer quality system, contractual obligations, and the EMS provider’s role. If ISO 13485 certification is required, state it explicitly and verify it during supplier qualification.

How early should an EMS partner become involved?

Ideally, before the design is frozen. Early review can identify manufacturability, test access, programming, component availability, panelization, fixture, labeling, and documentation issues while they are still easier to change.

Can Micron support research and hospital-affiliated development teams?

Micron has experience supporting electronics projects for area hospital research teams and other research-oriented programs. The best starting point is to share the build package, intended use, design maturity, quantities, test needs, and required documentation so the team can evaluate fit and scope.

What files should be included with the RFQ?

Send the BOM with manufacturer part numbers and approved alternates, Gerbers or ODB++, pick-and-place data, assembly drawings, quantities, target schedule, test and programming requirements, quality records, labeling, special processes, and any known regulatory or customer-specific controls.

Can an EMS partner help develop the test process?

Often, yes. The OEM should define what the product must prove, while the EMS partner can help evaluate test access, fixture concepts, programming flow, production sequence, data capture, and practical pass/fail implementation. Scope and ownership should be agreed before the build begins.

Explore Micron Capabilities
Start the Conversation

Bring the build package you have—and explain what is still changing

Micron supports prototypes, NPI, SMT, Through Hole, testing, programming, and recurring high-mix production from Norwood, Massachusetts. Share the product stage, BOM, PCB data, drawings, quantities, test intent, documentation needs, and schedule so the team can identify the clearest next step.

Browse practical EMS guidance, process articles, and Micron's ongoing insight series.

EMAIL OR CALL US
(781) 949-3500